FOOD PROCESSING
Empowering the Food Processing Industry with Safety, Efficiency, and Excellence
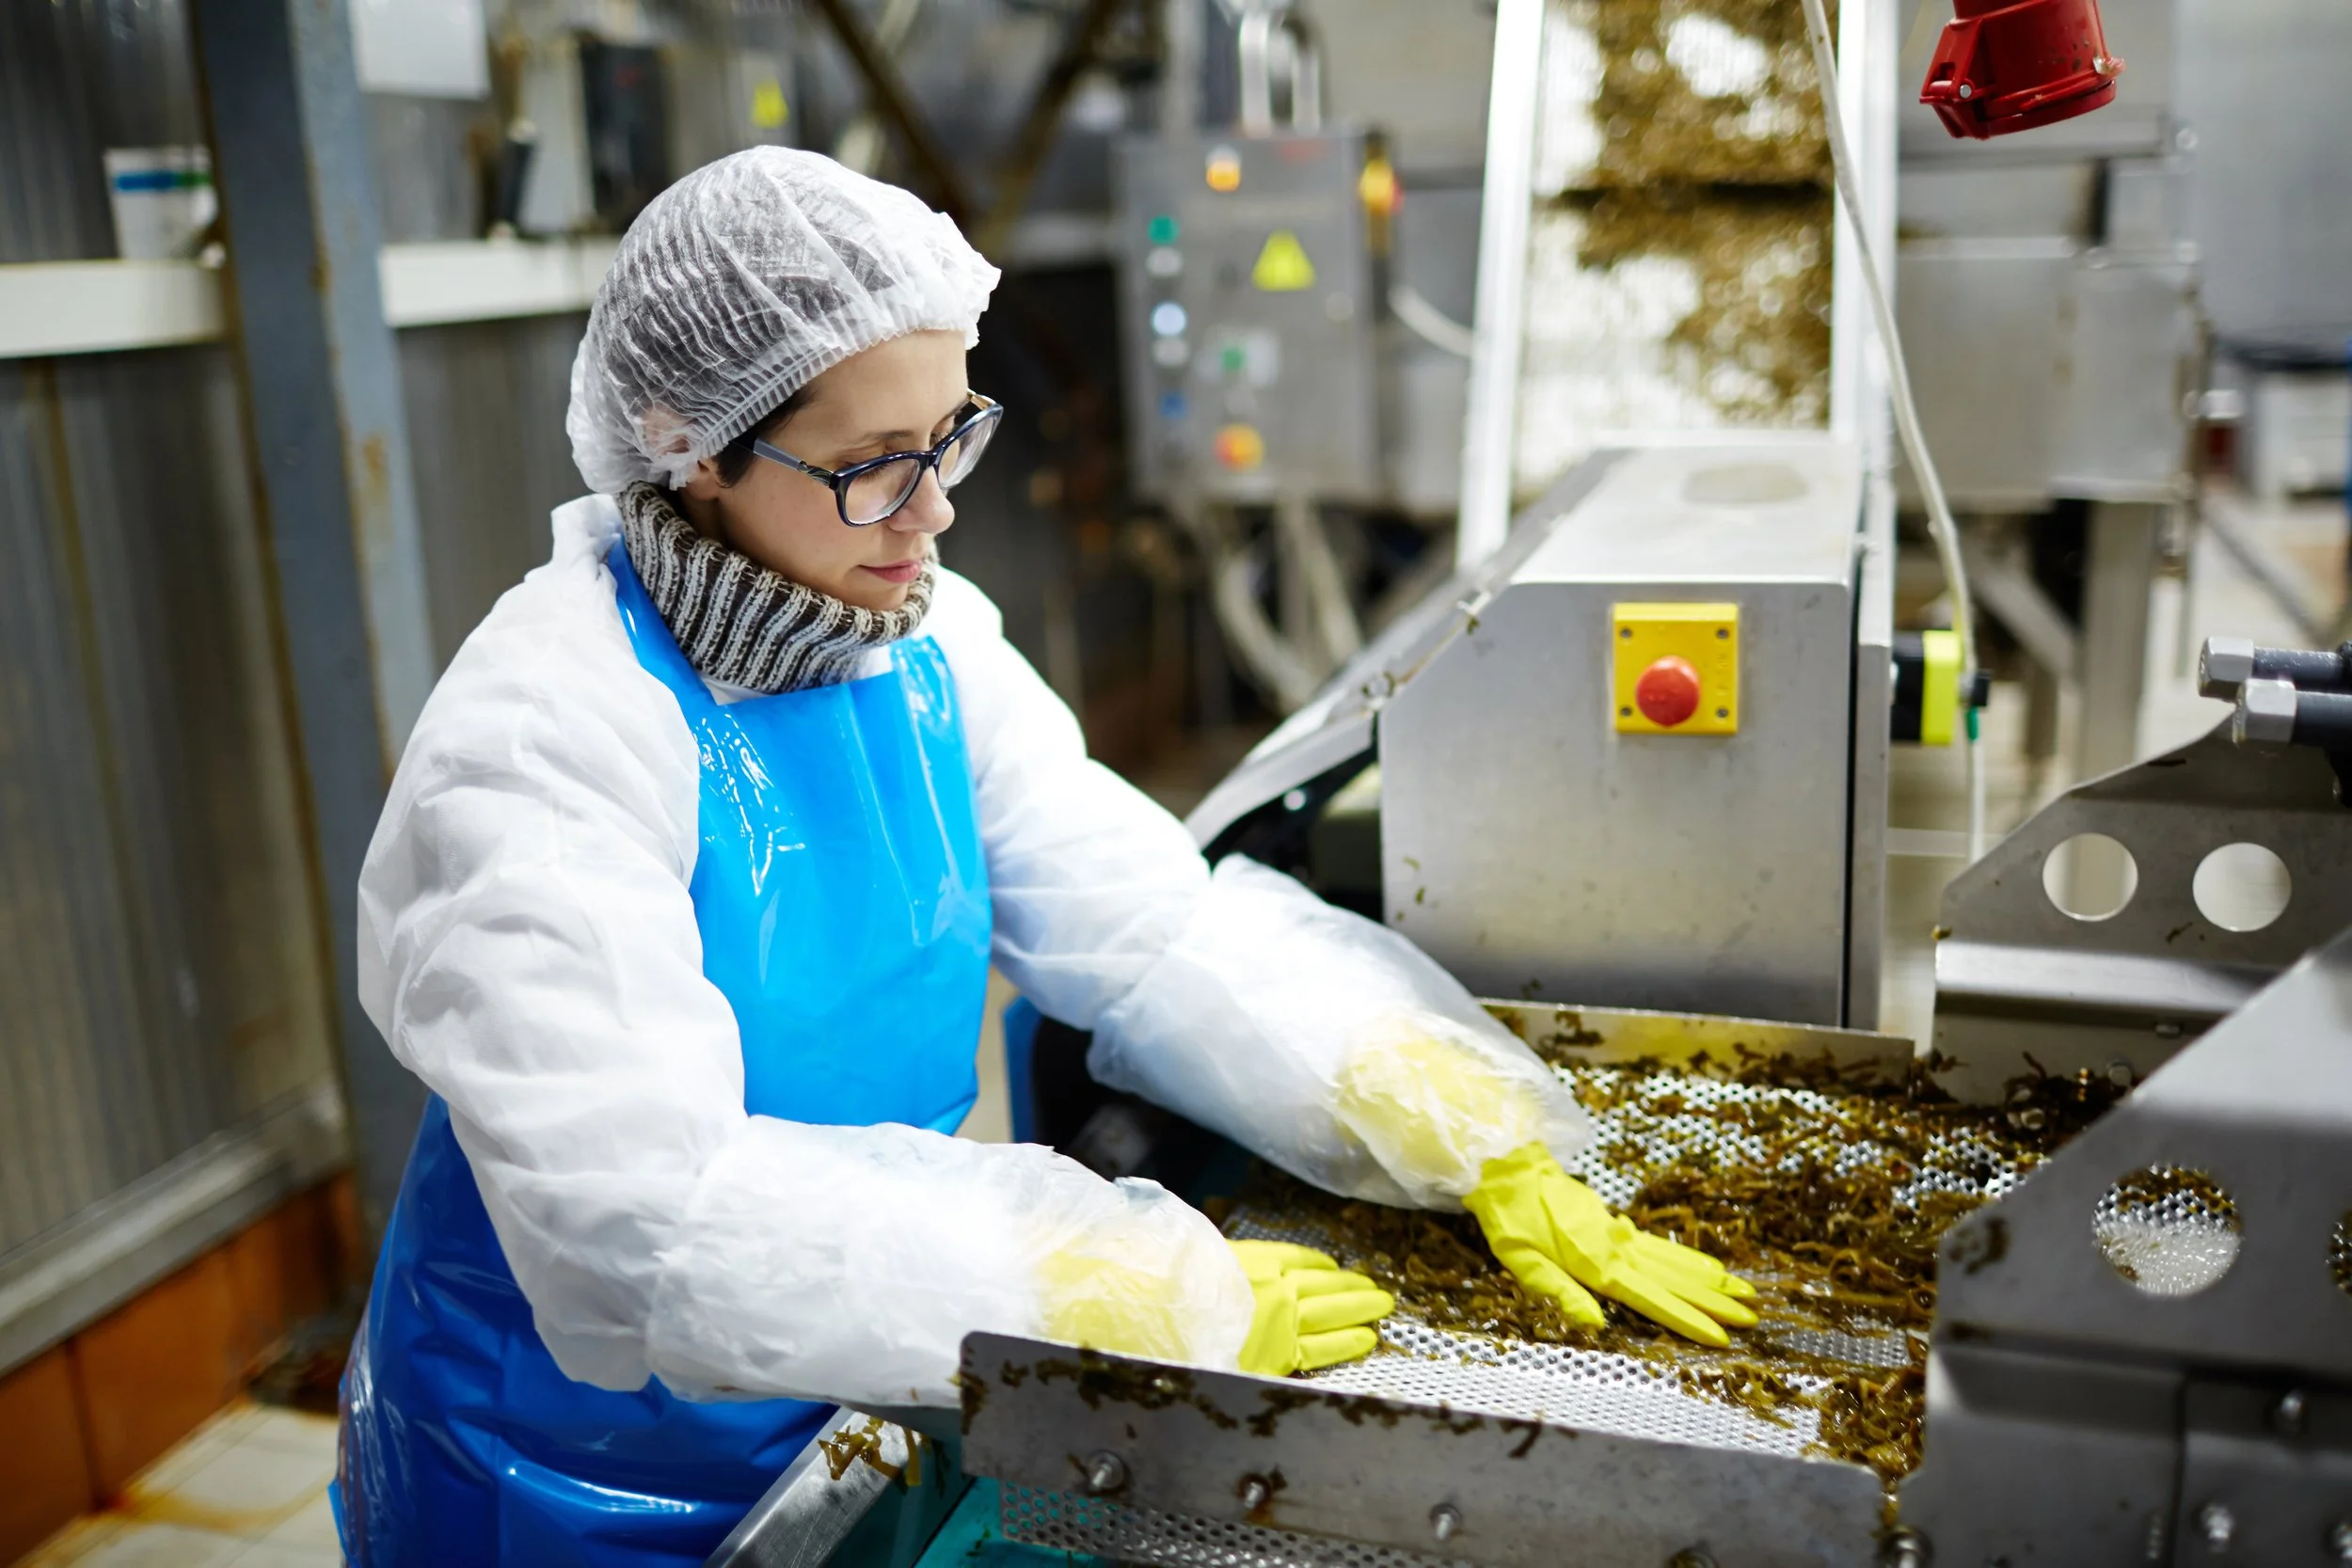
In the highly regulated food processing industry, the seamless integration of skilled personnel and well-maintained processing equipment is essential. Our team consists of associates ranging from quality control technicians to sanitation experts, each thoroughly trained in and committed to adhering to Good Manufacturing Practices (GMPs). Additionally, our maintenance services are designed to keep your production line operating smoothly, from preventative care for pasteurizers to emergency fixes for fillers, all while strictly following the critical boundaries of Hazard Analysis and Critical Control Points (HACCP) guidelines. This synergy ensures compliance with unwavering food safety standards at its core
Technical Solutions for Food Safety and Operational Excellence
Food processing demands an unwavering commitment to safety, quality, and operational efficiency. Our technical and operational solutions are tailored to meet these critical requirements across modern food processing environments. We support key functions including quality control, production operations, equipment maintenance, and sanitation processes, with a strong focus on food safety standards and regulatory compliance. Our integrated approach helps maintain product quality, improve operational reliability, and support safe and efficient production.
Maximizing Uptime for Large-Scale Food Production
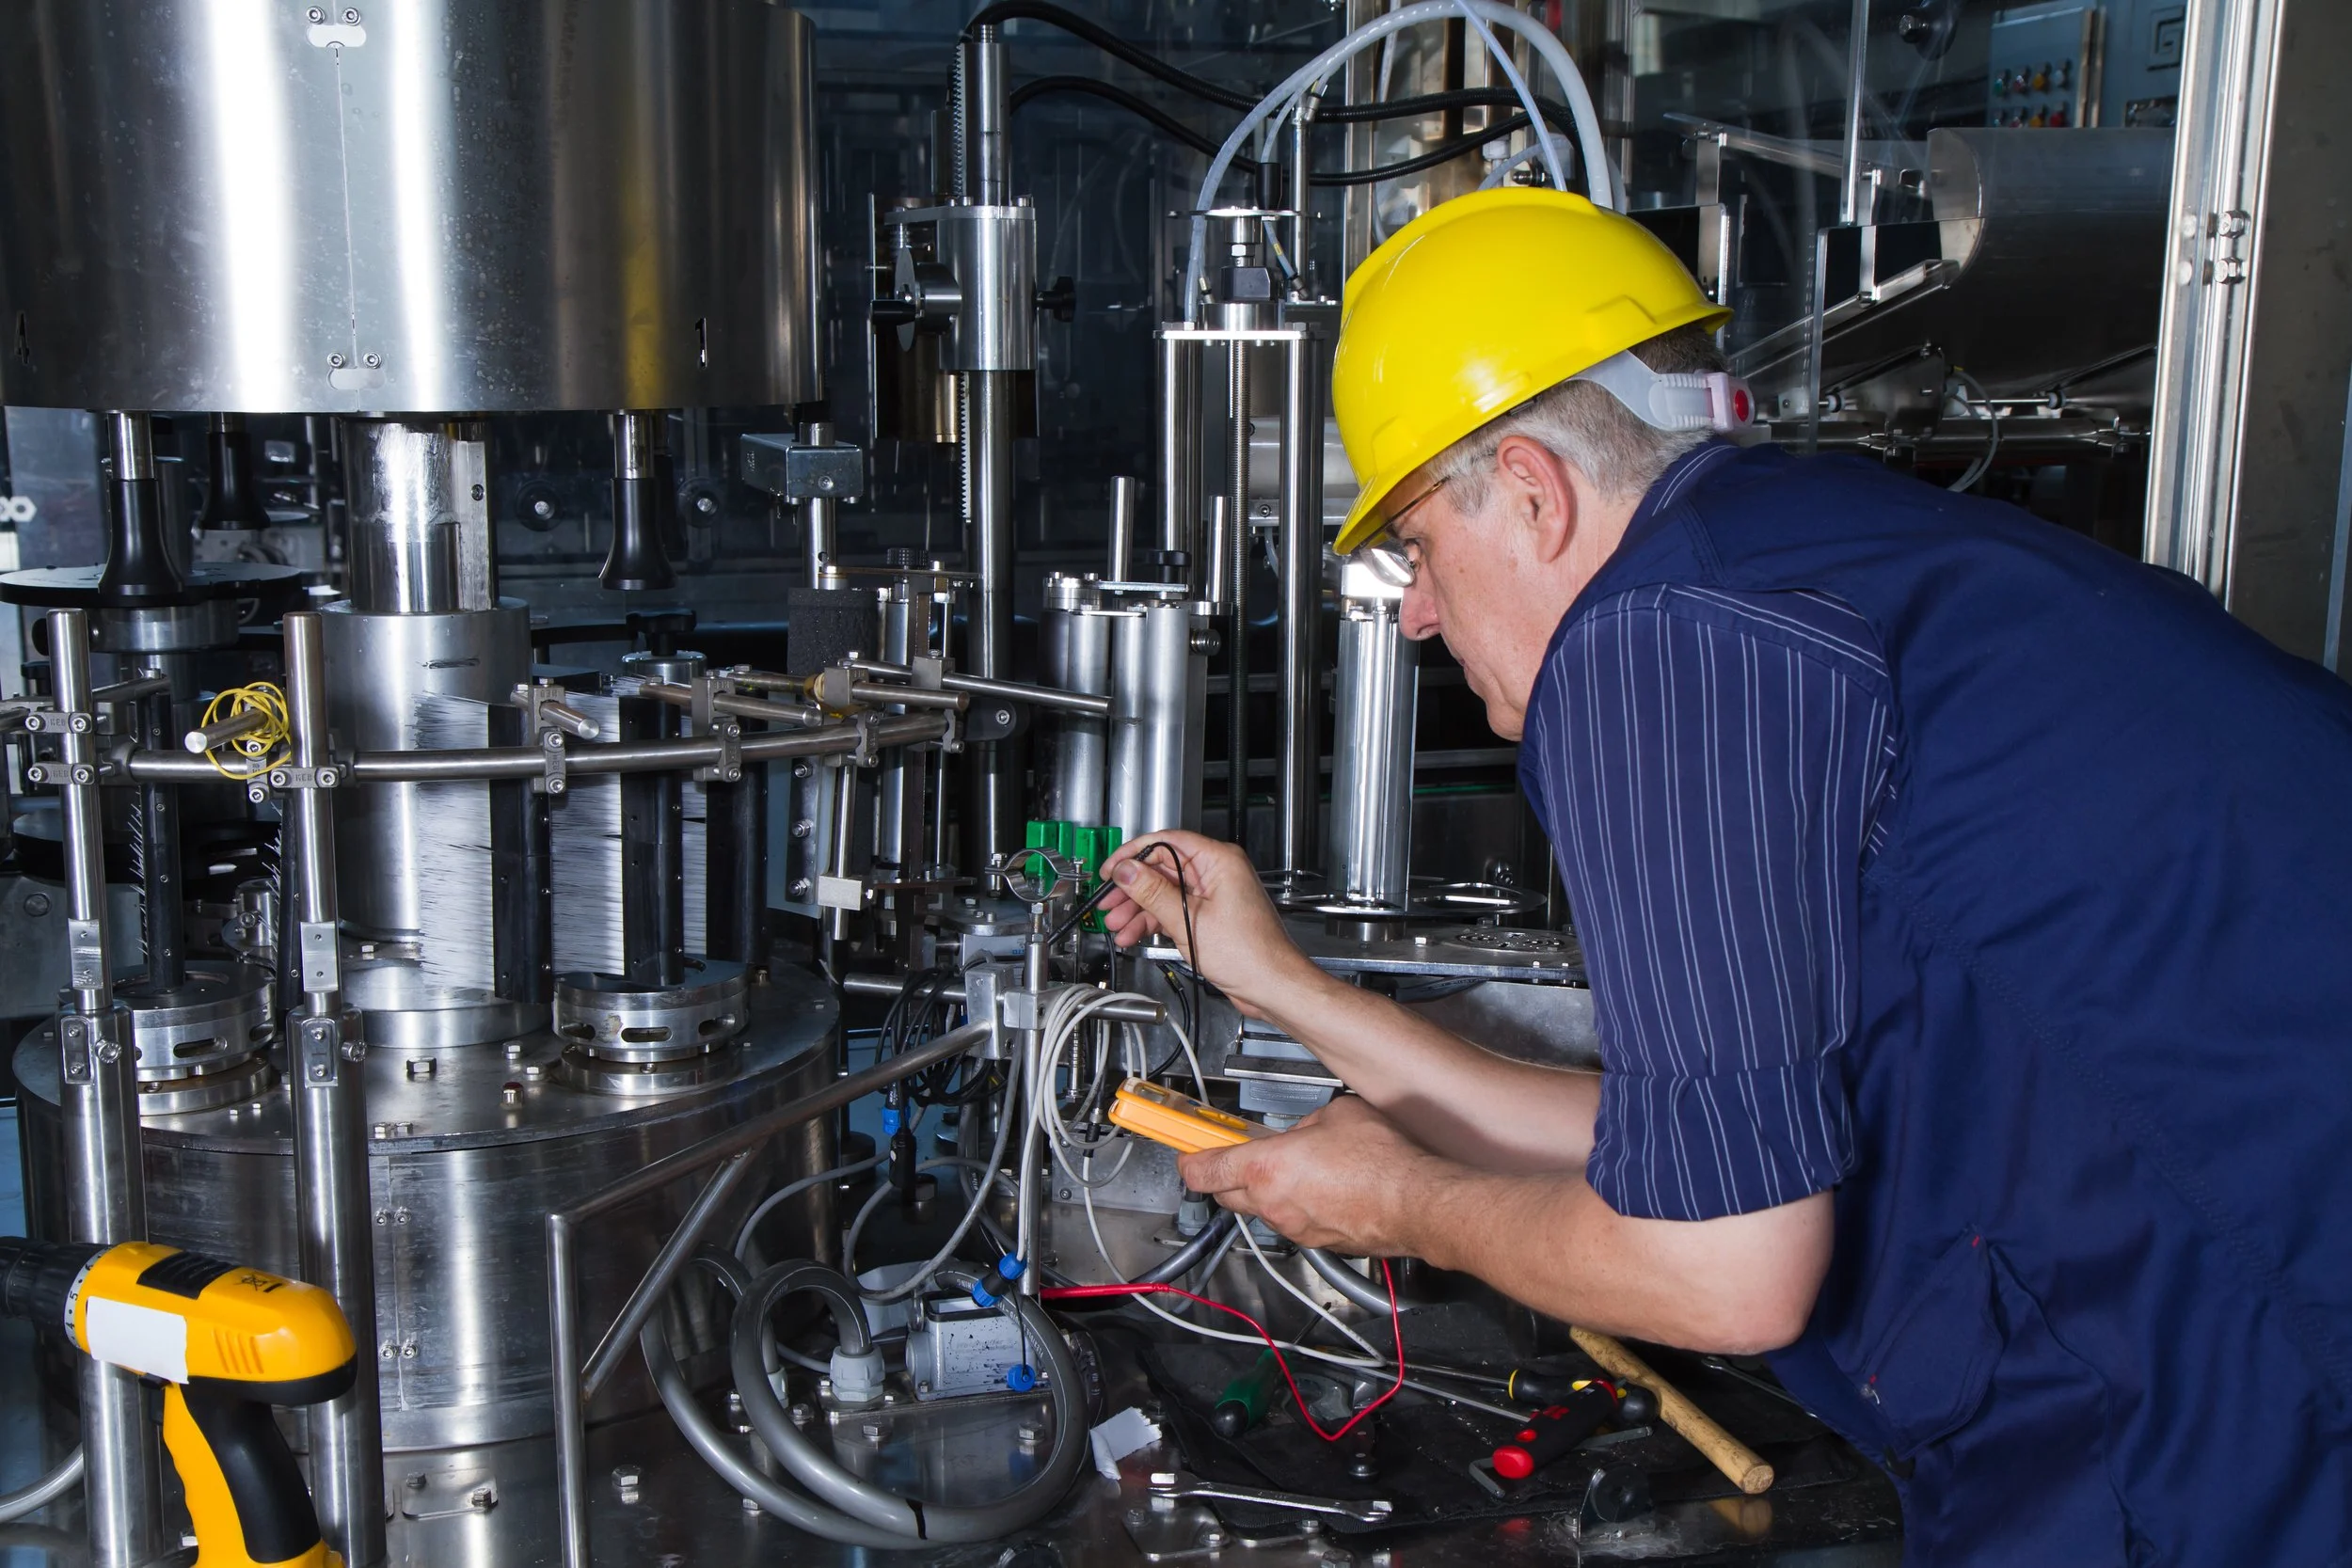
Large-scale food processing plants rely heavily on complex equipment like mixers, conveyors, packaging lines, and refrigeration systems. Our specialized maintenance services cater specifically to the food industry's needs for hygiene, safety, and operational efficiency. Experienced technicians provide routine maintenance, emergency repairs, and compliance checks to keep your equipment running optimally while meeting stringent regulations. By preventing downtime and extending machinery lifespan, our services enable continuous, compliant production at your large-scale facilities.
Tailored Technical Solutions for Your Operational Needs
In the demanding food production environment, safety, quality, and operational consistency are essential. At Zeniq Tech, we provide technical and operational solutions tailored specifically for food manufacturers. Our capabilities include:
HACCP & Food Safety Support
Quality Assurance & Quality Control
Sanitation & SSOP Compliance
Packaging Equipment Operations
Processing Line Operations
Our services are designed around the unique requirements of food processing environments, supporting critical functions that maintain high standards of hygiene, safety, quality, and operational efficiency. From HACCP-based quality control and SSOP sanitation practices to packaging and processing line operations, our integrated approach supports regulatory compliance, reliable production, and consistent operational performance.
Comprehensive Machine Maintenance for Uninterrupted Operations
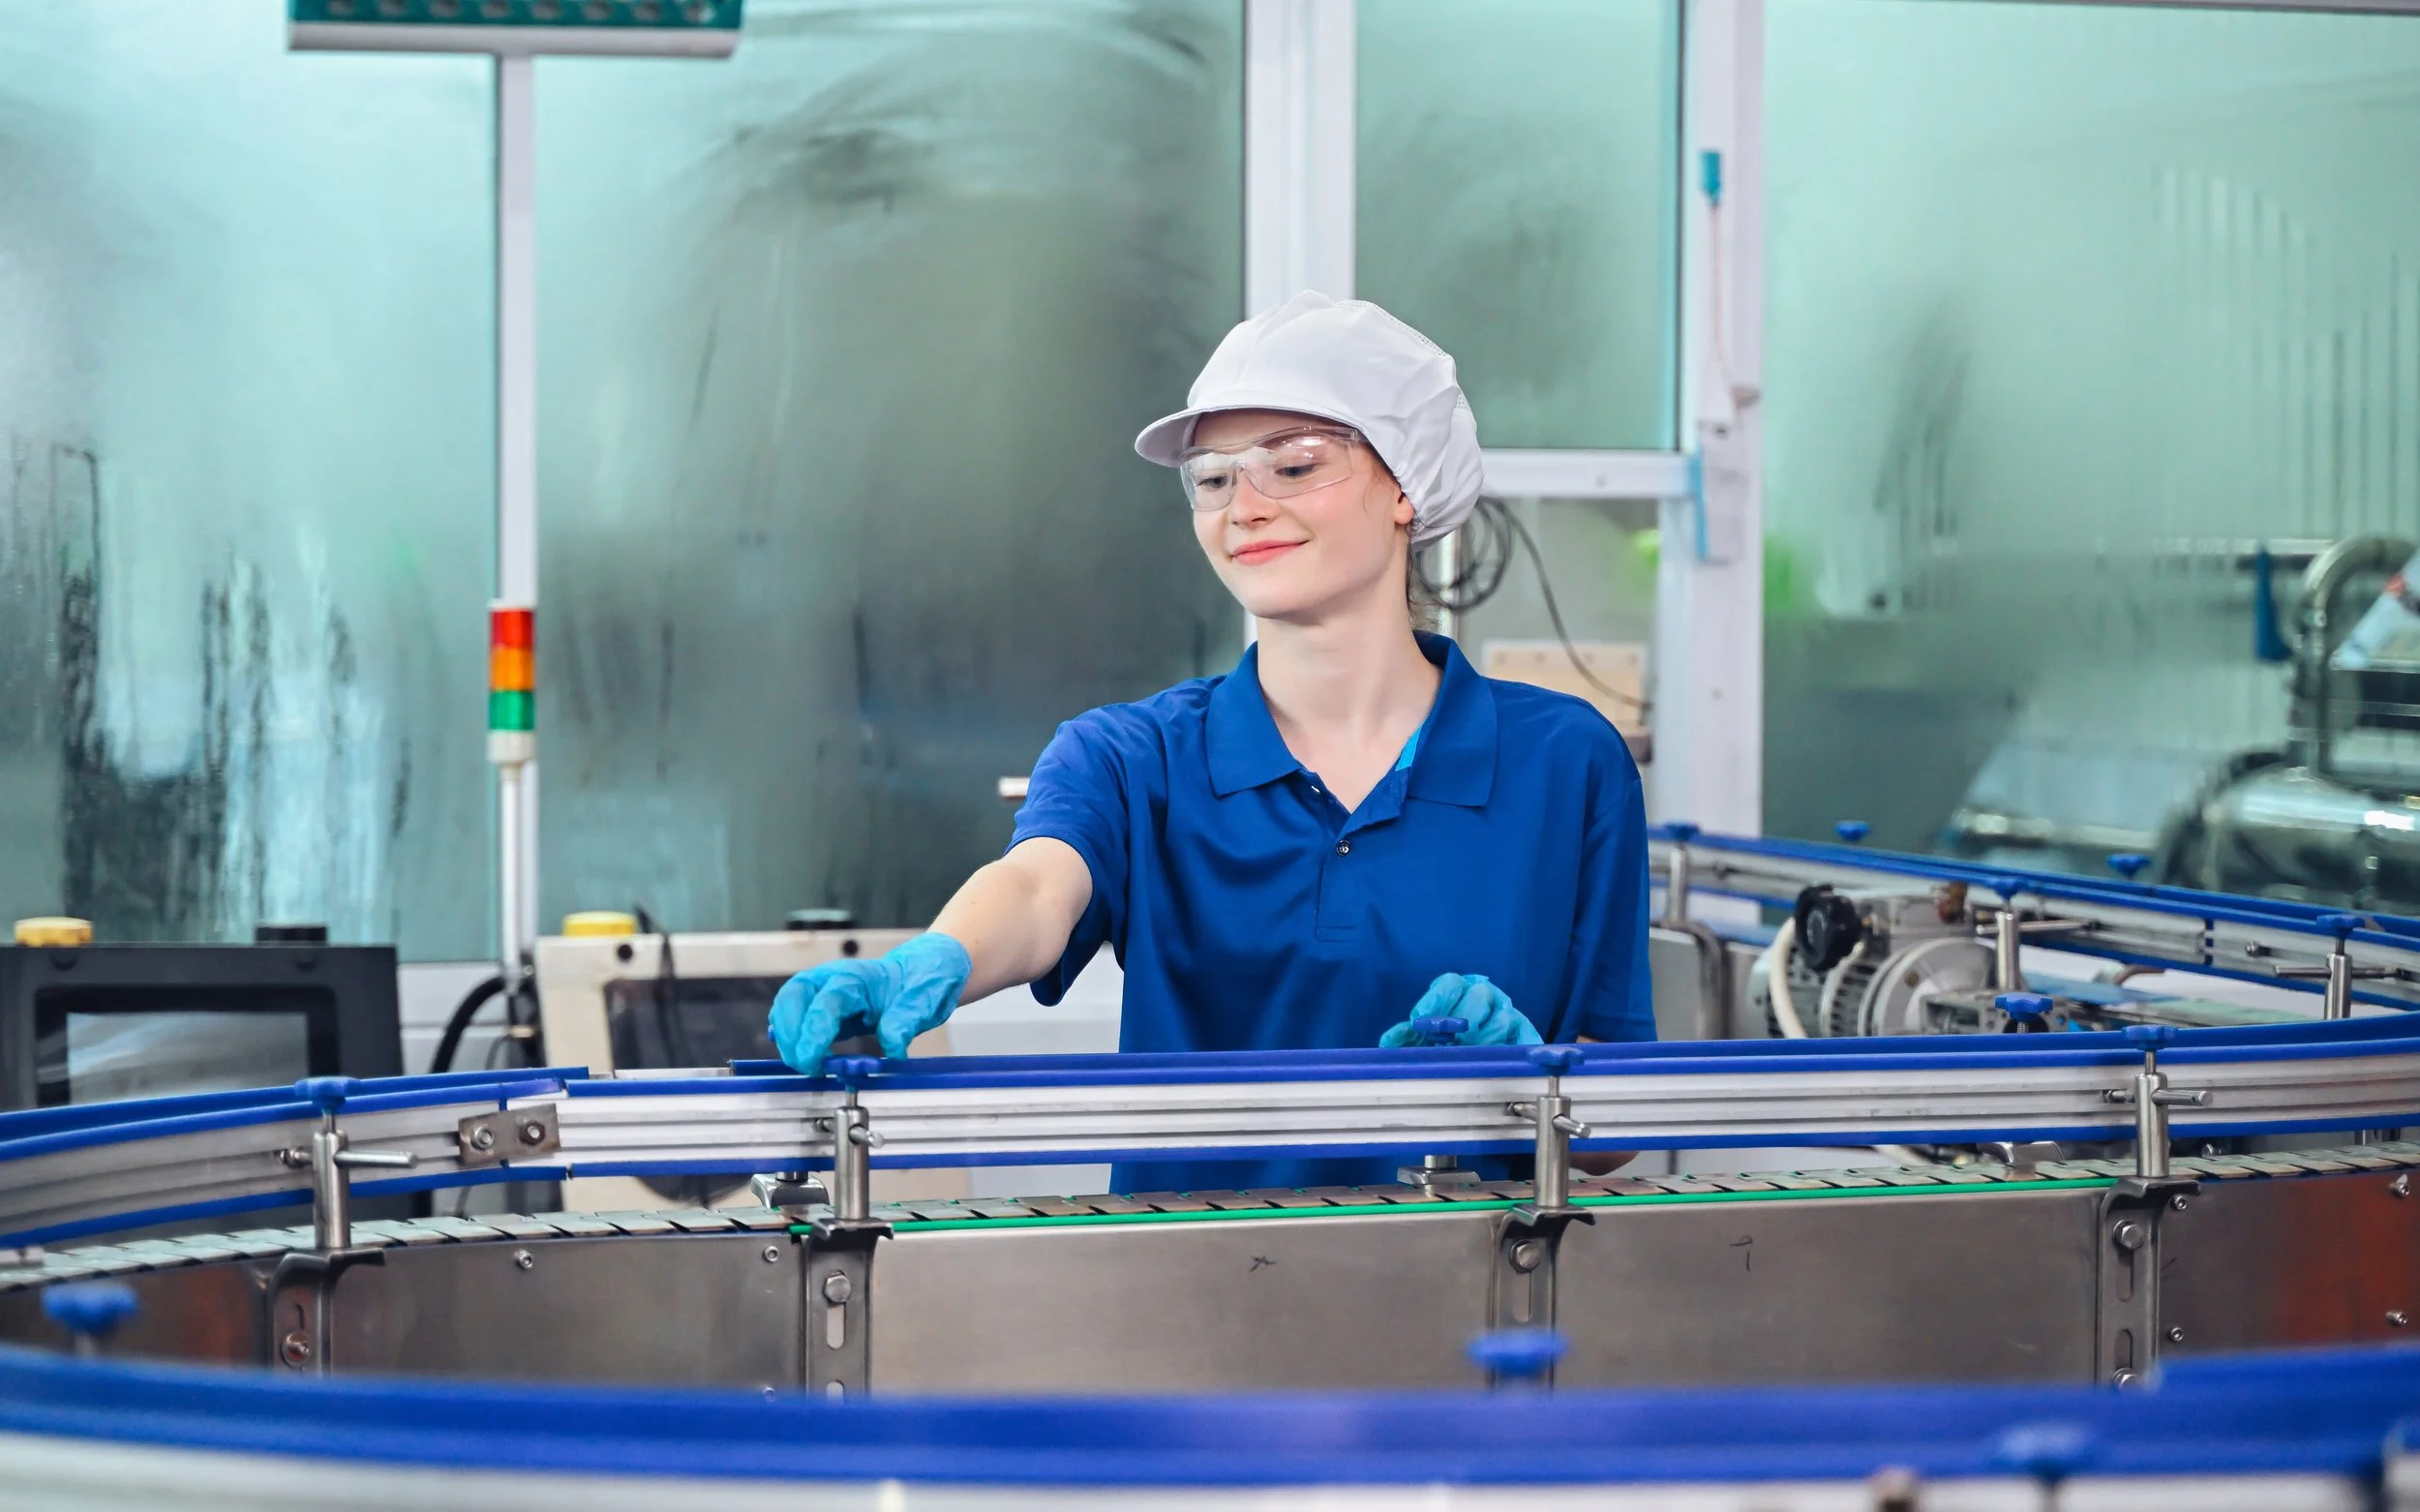
Unplanned downtime disrupts production schedules and hurts your bottom line. Zeniq's comprehensive Asset Reliability Services provide turnkey maintenance solutions:
Preventive Maintenance Planning
Predictive Maintenance Technologies
Emergency Breakdown Support
OEM-Trained Technicians
Compliance Audits
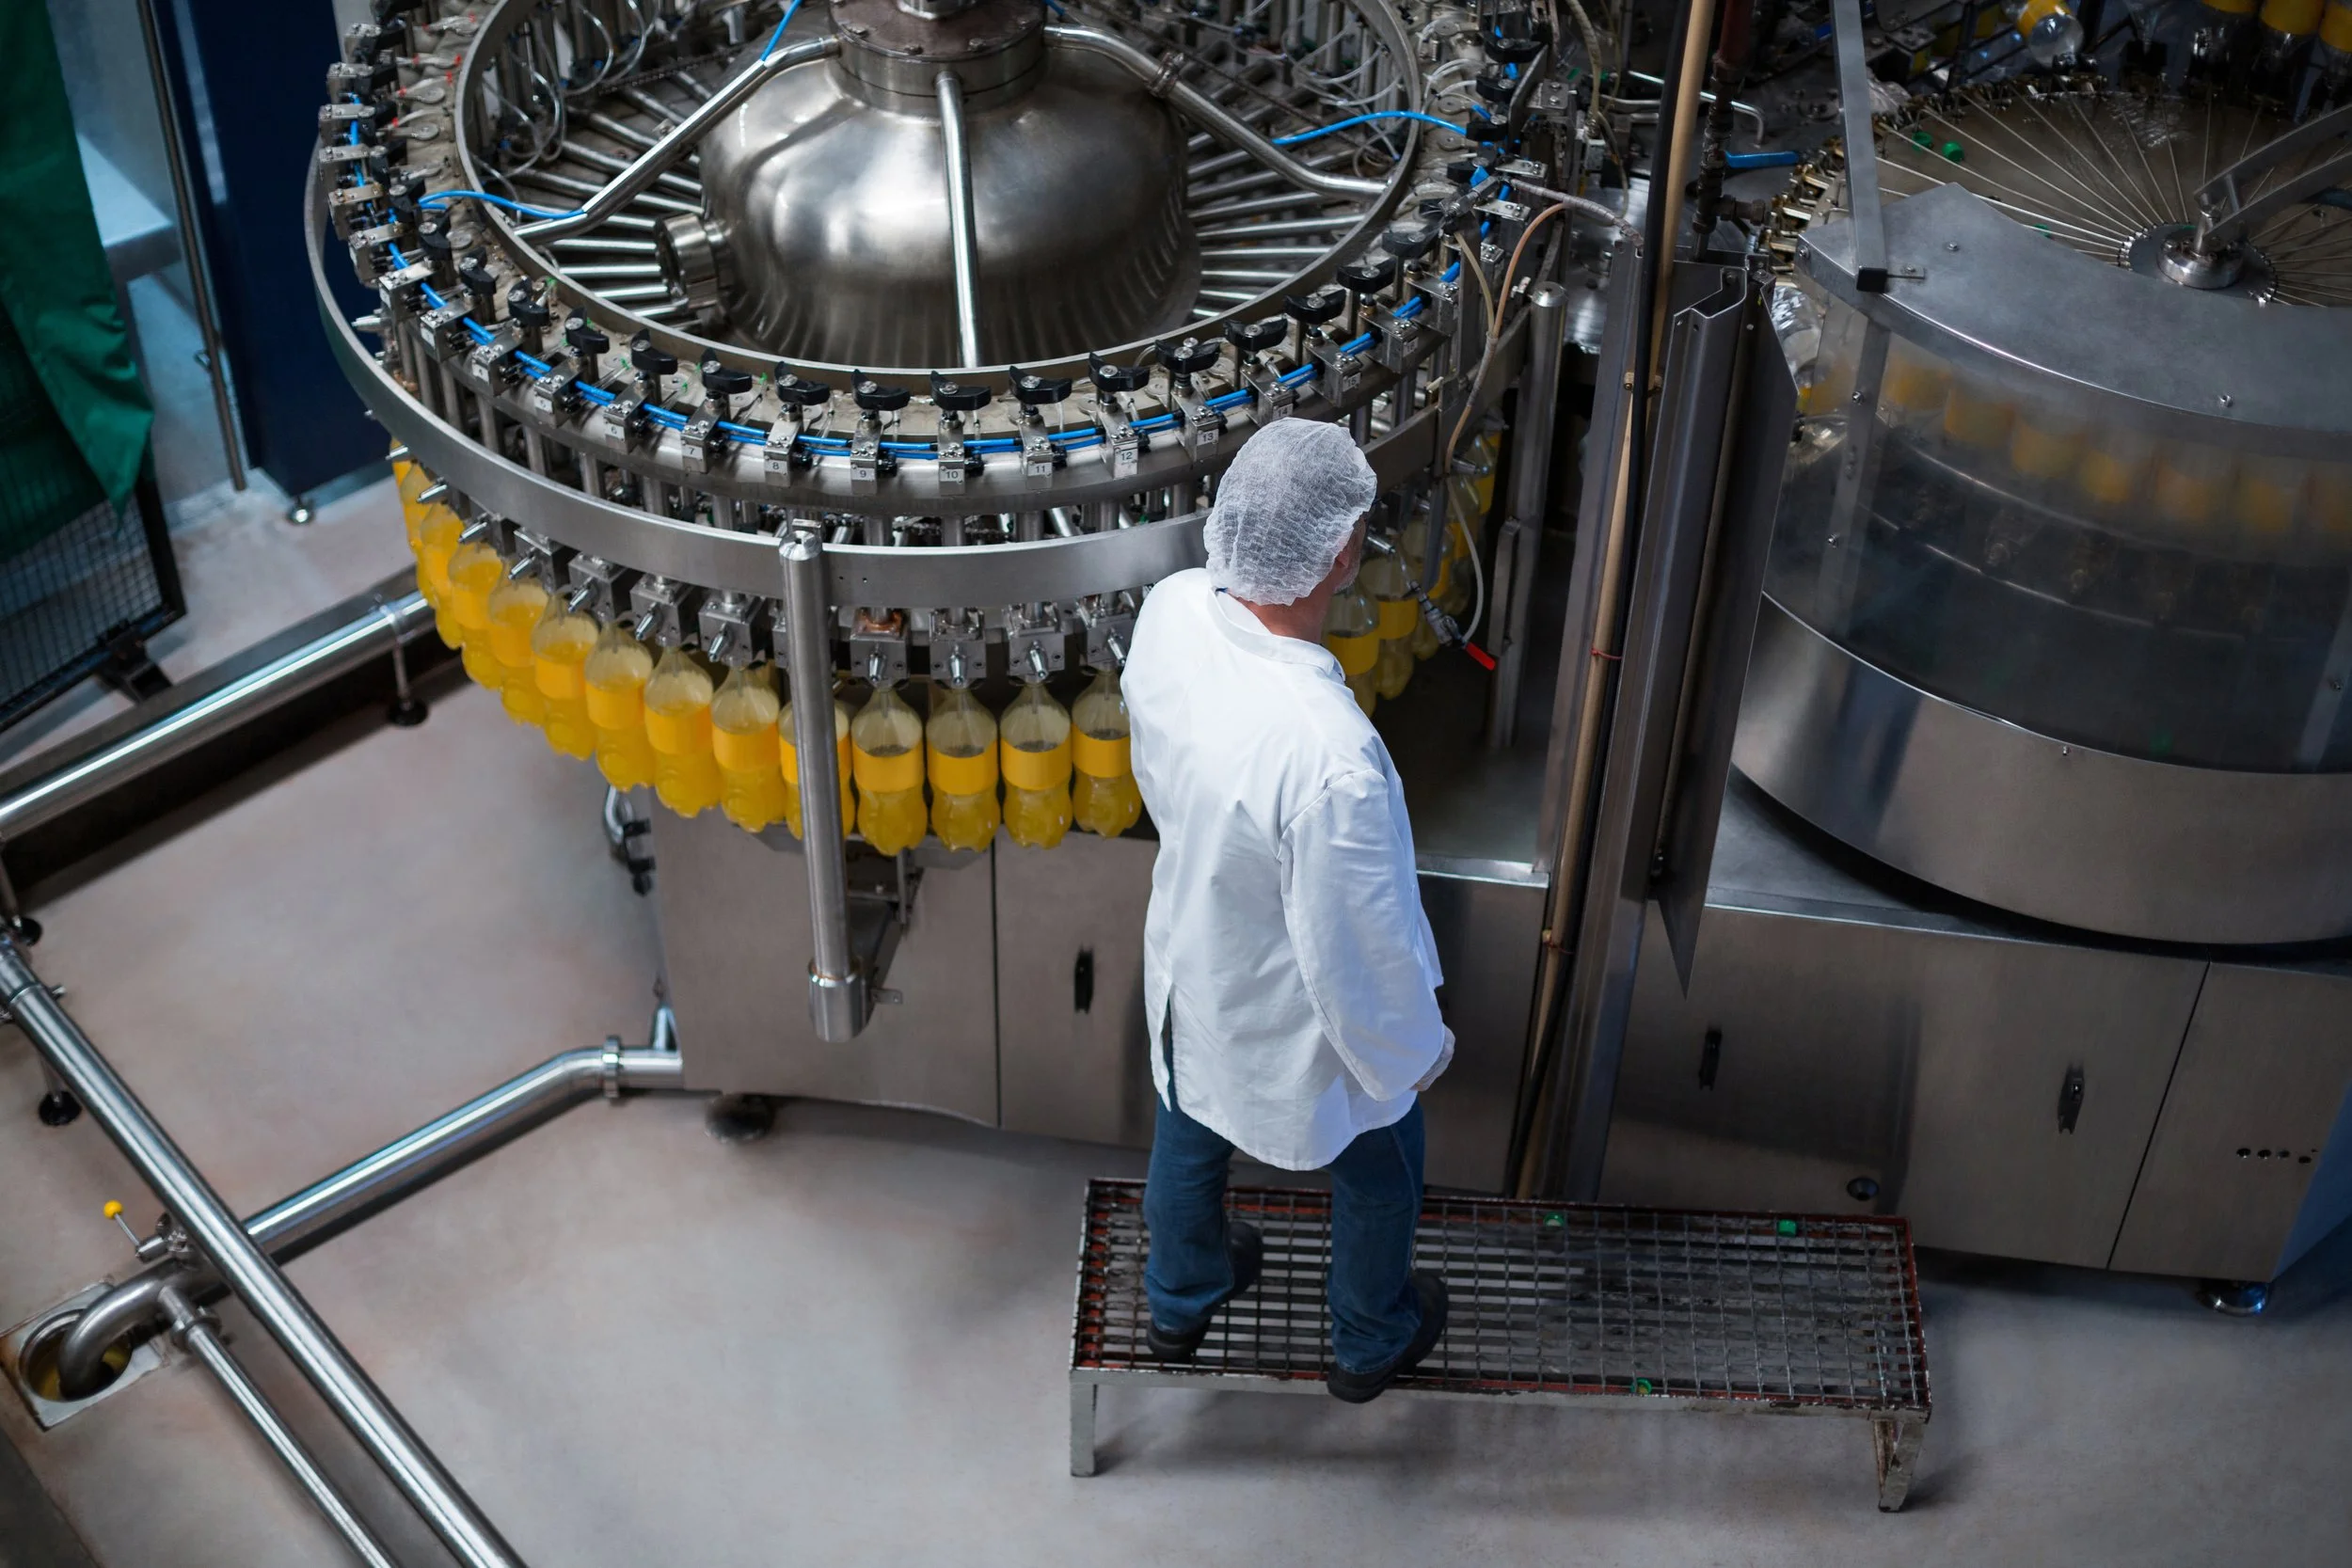
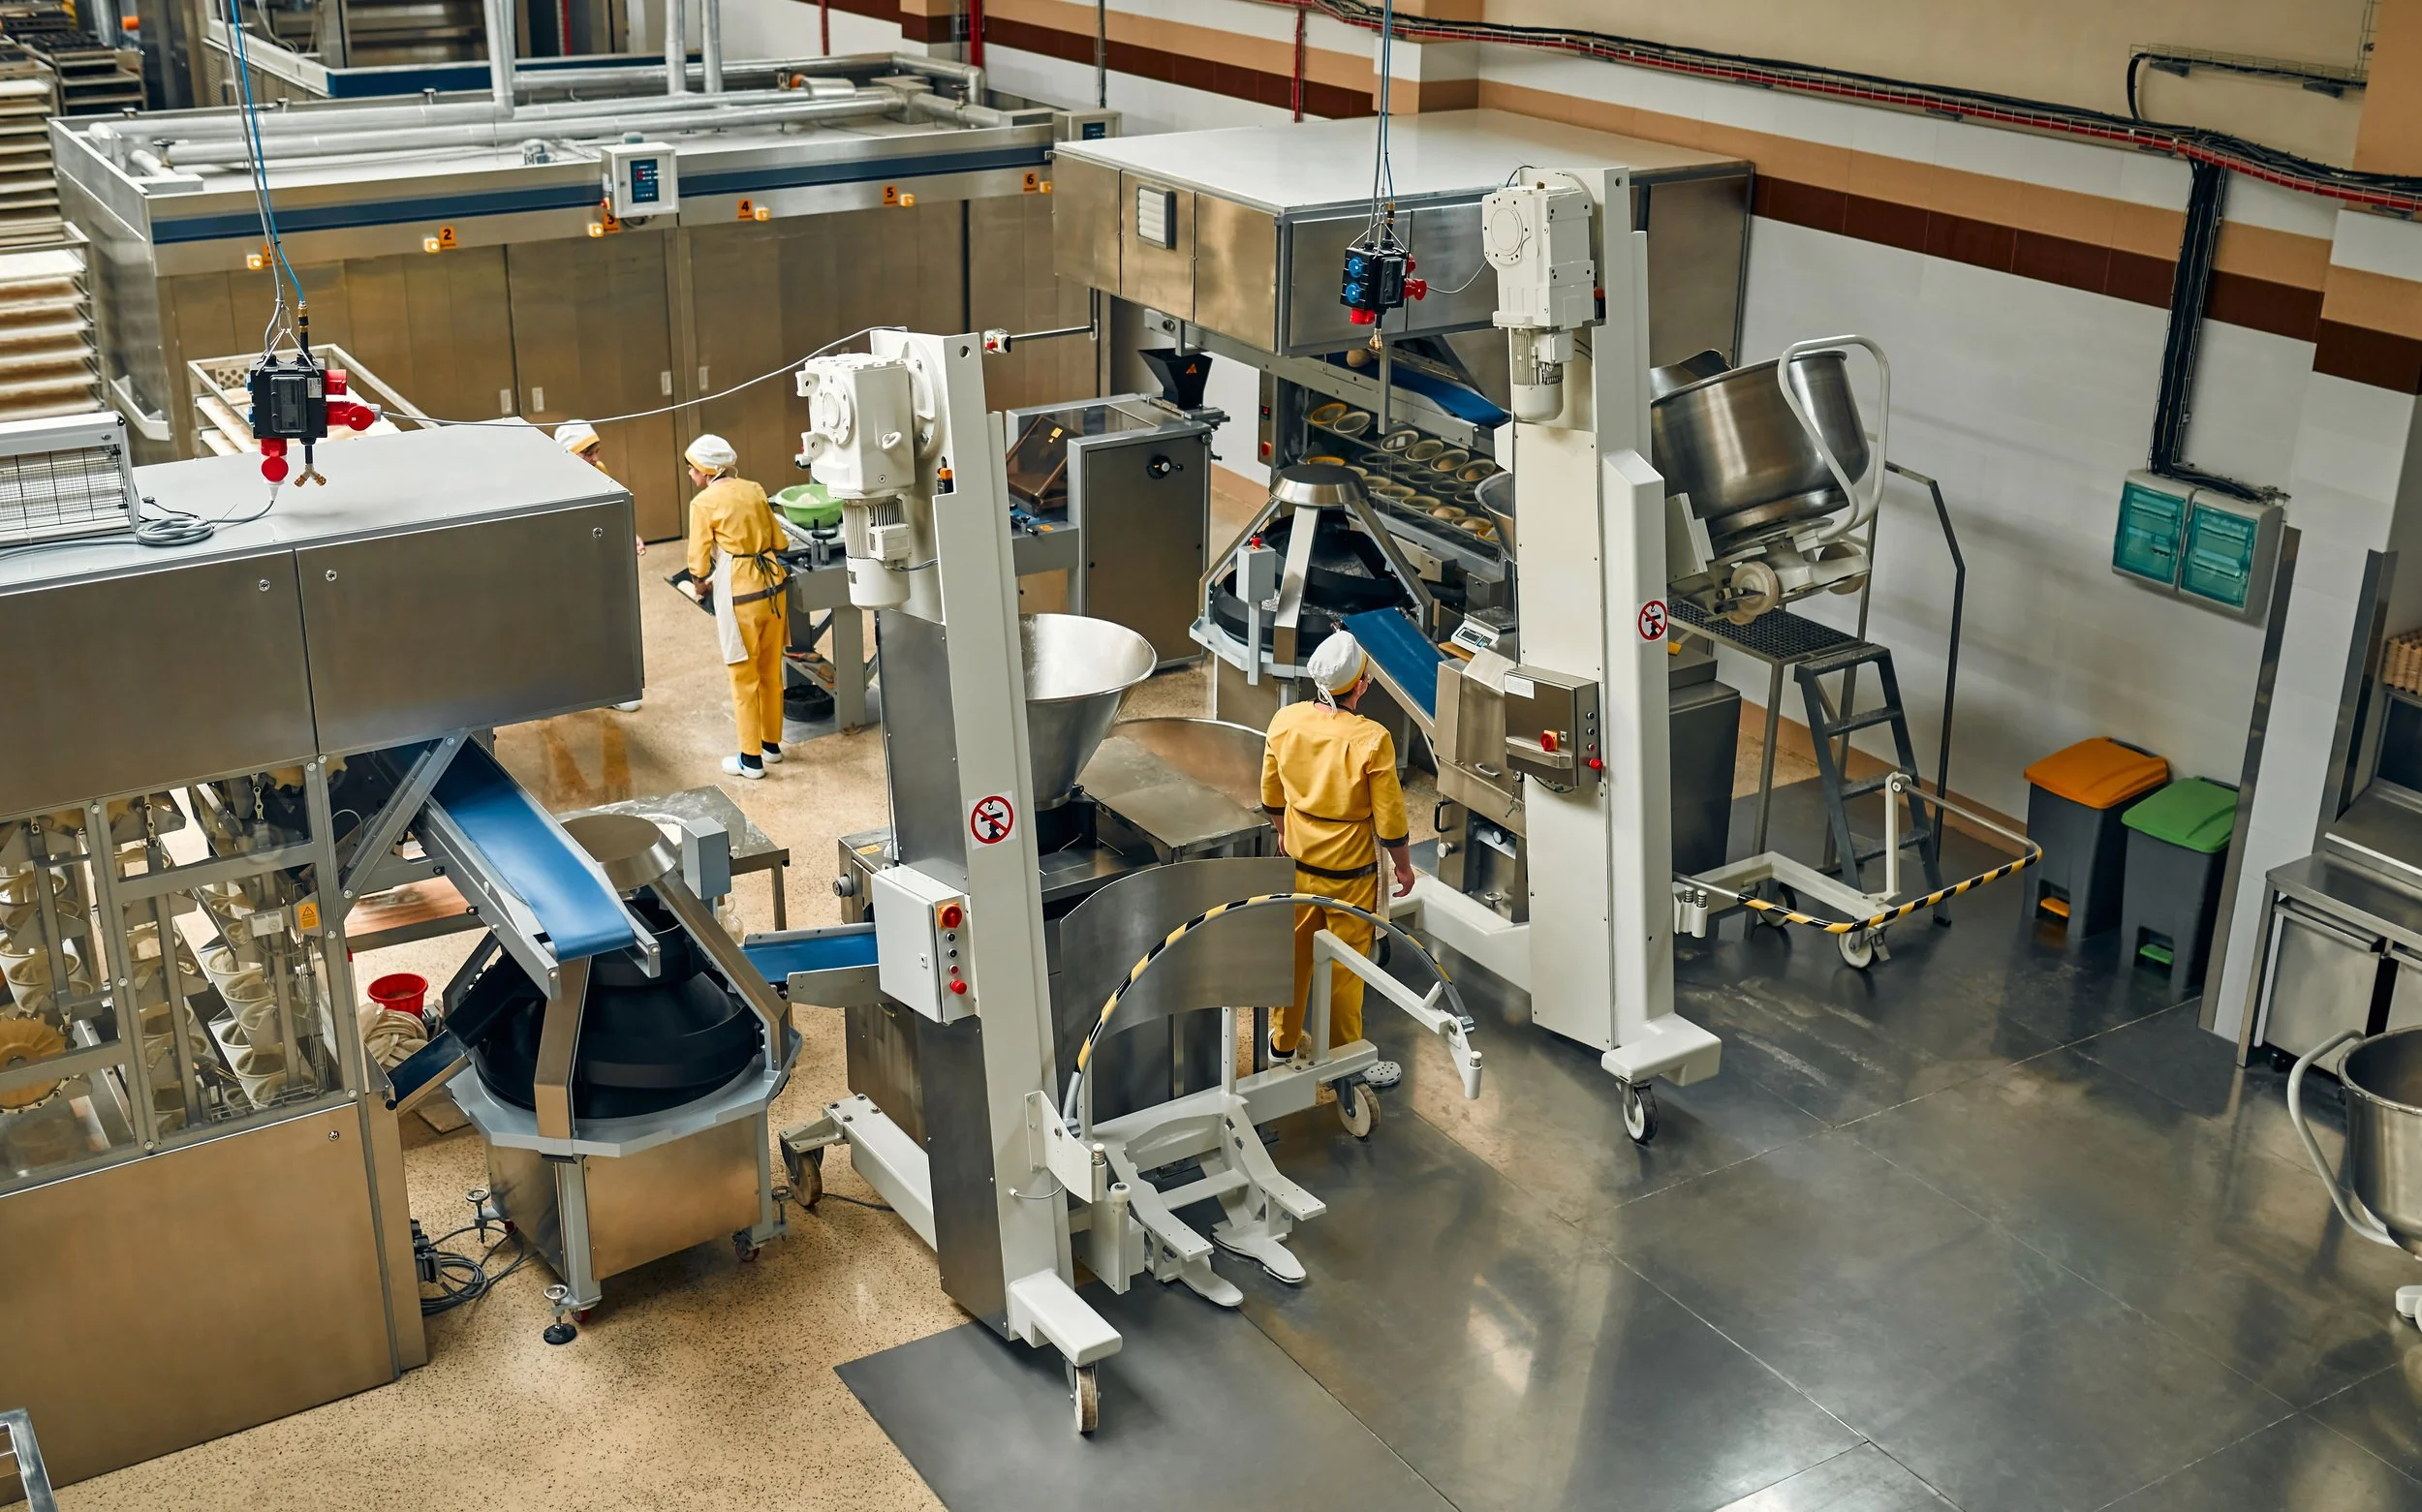
Opt for our outsourced maintenance service, and gain peace of mind knowing every gear and conveyor in your operation adheres to the highest operational and safety standards, including stringent GMP compliance. Whether it’s routine servicing of your fillers and pasteurizers or urgent repairs on your conveyance systems, our maintenance solutions are there to ensure minimal downtime and maximal productivity.
Flexible Service Models to Fit Your Needs
At Zeniq Tech, we recognize that one size doesn’t fit all. Choose our comprehensive machine maintenance services for complete equipment care, or select flexible technical and operational support tailored to your specific requirements. Whatever your needs, our services are scalable and adaptable, designed to address the unique challenges and evolving demands of your food processing operation.